Mistakes to Avoid When Choosing a WIA Welder
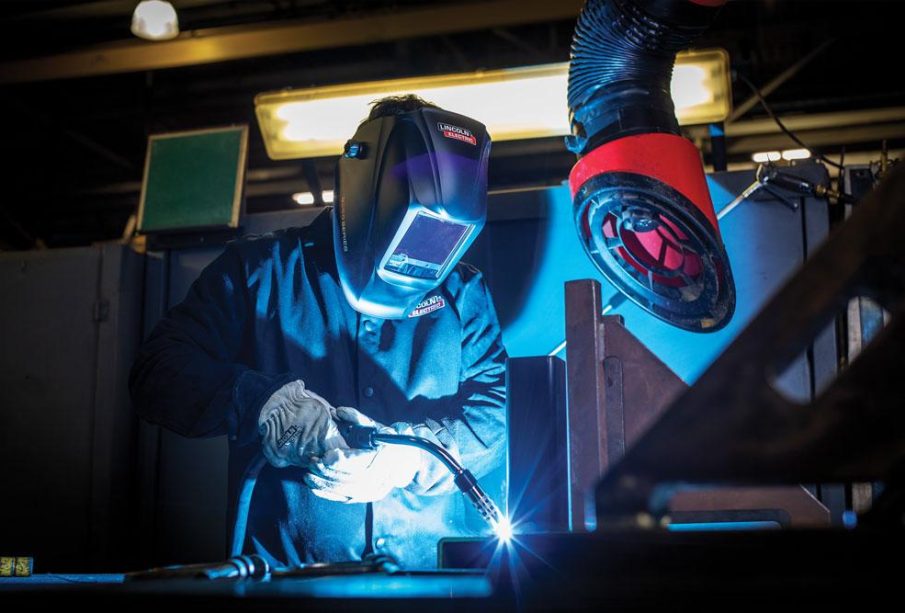
Most buyers walk into a welding purchase thinking about amps. A better starting point is how that welder will be used day after day, and what it costs to keep it running.
Chasing peak amps and skipping duty cycle
The number on the front gets all the attention. A 200-amp sticker looks better than a 170-amp sticker, but that number means little on its own. What counts is duty cycle at a given amperage before heat forces a stop. That’s the real limit.
Duty cycle is rated over a 10-minute window under AS/NZS 60974-1. A rating of 25% at 200 amps means about 2.5 minutes of arc time followed by about 7.5 minutes of cooling under the maker’s test conditions. Actual shop results shift with airflow, ambient heat, extension leads, and how hard the machine is pushed. Thermal overload protection will cut output when limits are hit. New buyers often read that shutdown as a fault.
Check the fine print on ratings
Ratings assume specific test conditions that shops don’t always match. Poor ventilation and long supply leads pull usable duty down, as does high heat in the shop. The manual states the conditions behind the numbers. Read that page before comparing brands.
Maximum amps also hide the other end of the range. Thin sheet and small tube need low, stable minimum output. A machine that starts at 40 amps will fight thin auto body panels. A machine that drops to 15 or 20 amps gives far more control on that work. Buyers who weld mostly under 6 mm rarely touch the top of the dial.
Buy the output that fits the work.
Don’t compare a 200-amp rating at 15% duty with a 170-amp rating at 60% duty as if the bigger number wins. The second rating allows more arc time at its stated output under the specified test conditions. Whether that improves productivity depends on the process, joint, required current, and work pattern.
Picking a machine before picking a process
Many shoppers start with catalogs and end with confusion. They compare multi-process units before they know what process the job needs. That order burns cash. Process comes first, followed by output and extras.
MIG suits most light fabrication. It handles mild steel sections and runs fast, and it’s easy to learn for straight joints. TIG fits a different need. It gives cleaner control on thin material and neat finishes where appearance counts.
Buyers who want TIG often miss two details. They don’t check if the machine runs both AC and DC for steel and aluminum, or how gas flow is controlled at start and stop. Those details decide if TIG is usable or just a badge on the panel.
Stick still has a place for outdoor repairs and windy sites where gas cover blows away. It tolerates less-than-clean steel better than gas-shielded processes. That does not mean painted, coated, or oily metal is safe to weld as found. Coatings and fumes can be hazardous, so surface prep, extraction, PPE, and training need to follow maker guidance and qualified safety advice.
Material thickness usually settles the choice, since thick plate points one way and thin sheet points the other. A multi-process unit carries dead weight if two modes stay dark. Pay for modes that match actual jobs in the next year or two.
Assuming any welder plugs in at home
Home garages run on single-phase supply. Some larger workshop units need three-phase supply to run at rated output. Skipping that check stalls the job.
Input requirements live on the rating plate and in the manual. They vary by model and rated output. A qualified electrician should assess what the building supply can support before purchase. Don’t guess from plug shape or current class alone.
An upgrade can involve new wiring and supply capacity as well as a different socket. That work needs a licensed trade and time on the schedule. It hurts to pay for it after the welder is already on the floor. Small shops in older buildings face this most, as the supply that runs lights and hand tools won’t always carry a high-output welder under load.
Think about where the welder will live. A home garage and a rented industrial unit have different limits. The safe move is to match the short list to the actual site early, with input from the electrician and the dealer.
Sales talk makes this worse. Phrases like industrial power or workshop ready mean nothing without the volts and phases on paper. Get the input volts and phases in writing and hand them to the electrician for review.
Shopping on price without local backup
Online prices are hard to ignore. A saving of a few hundred looks smart on screen. It looks less smart when drive rolls wear and no one local stocks the right parts.
A local dealer does more than sell the box. The good ones keep tips, liners, drive rolls, and torch parts on the shelf. They have a bench that can test boards and feed systems, and they answer the phone when wire starts acting up.
If the short list points to a WIA machine, price is only half the question; if you settle on a wia welder, make sure your dealer can demonstrate it and stock genuine consumables, with service available after the sale.
Genuine consumables fit as designed. Copy parts can throw off feed and arc stability. A dealer that services what it sells shortens downtime because diagnosis starts from known parts.
Distance makes this matter more. Freight each way for a warranty job eats weeks. A shop that is hours from help can’t afford that loop for a simple feed fault.
Ask how warranty claims are handled and where the work is done. Ask what the usual turnaround is for a board check. Vague answers at sale time turn into slow answers later.
Mistaking feed faults for machine faults
Birdnesting stops a job cold. Wire bunches up before the drive and nothing reaches the torch. Burnback looks different: wire fuses to the contact tip and the arc dies at the tip.
Both faults point to the feed path more often than the power source. Liner and tip size must suit the wire type and diameter. Drive components must suit them as well. A small mismatch creates drag, which leads to heat and slipping. That can end in a tangle or a fused tip.
New owners often blame the welder and start twisting knobs. That wastes time. The fix starts with maker guidance for the exact wire and torch combination. If doubt remains, a dealer service bench can check the setup against spec.
Know what steady feeding needs
Dust and worn tips make feed faults more likely. Poor wire storage does too. Use only the consumables listed for the torch. When feed faults repeat, treat them as a setup issue to be checked, not a power fault to be cranked through.
Aluminum wire and flux-cored wire behave differently in the same liner. One is soft and marks easily. The other can be less forgiving of poor fit. Don’t assume settings carry over when the spool changes. Check the maker’s chart for the new wire and consult the dealer if symptoms persist, since forcing wire through a path only wears parts faster and wastes time on rework.
Going gasless just to avoid the cylinder
Gas cylinders feel like a hassle. There is cylinder hire, refills, transport, and storage. Flux-cored wire promises a way around all that. No bottle means faster setup.
Gasless has its uses. It works well where wind strips gas cover and lays down strong welds on heavier sections. Spatter levels rise quickly, though, and bead profile is harder to keep neat.
Gas-shielded MIG with an argon and carbon dioxide mix gives cleaner arcs on fabrication work. Beads sit flatter and spatter drops, reducing post-weld grinding. The cost is ongoing. Cylinder hire and gas use sit in the background of every job.
Don’t assume gasless means no safety gear or ventilation. All arc processes produce fumes and glare that demand PPE and ventilation per maker guidance. A demo that runs the same joint with both wires tells more than any brochure. Watch the arc and the cleanup time.
Wire diameter matters as well, since thin wire at low output suits sheet while thicker wire suits heavier plate, and the wrong match burns through or lacks fusion. Choose wire for the jobs on the bench, not the invoice on day one. Thin panels and visible joints favor gas. Outdoor repairs on thick plate lean the other way.
Buying too much machine and too few accessories
A big industrial unit impresses. It also costs more to buy and run. Low-end control suffers on machines built for thick plate all day, making thin work twitchy. A hobby shop that buys 500-amp capacity for weekend brackets pays for power it never uses.
The reverse hurts too. An entry unit pushed into production work hits thermal limits fast. The fan runs nonstop and output sags, while boards and torches live hot. That shortens service life and wipes out any savings from buying small.
The welder is only part of the ticket. A regulator and gas come first, with spare wire close behind. Then safety gear. An auto-darkening helmet and gloves are baseline, not extras. Freight and clamps add more. Buyers who budget for the box alone stall before the first weld.
Build a ready-to-weld list
Match both ends of the amperage range to the work. Check the lowest stable amps for sheet as closely as the highest amps for plate. A machine that covers the middle of the daily workload with duty to spare will beat an oversized unit that idles at the bottom of its dial, and it will feel calmer in the hand during long runs on light sections.
Ask the dealer for a ready-to-weld quote. It should list the machine and torch setup to suit, along with gas needs and safety gear in one place. That sheet shows the real spend. It also stops the classic error of a new welder with nothing to feed it.
A good purchase feels boring. The machine fits the process and the power without drama. The dealer answers and the spares are on the shelf. The arc behaves as expected.